CE · RoHS
Test report per batch
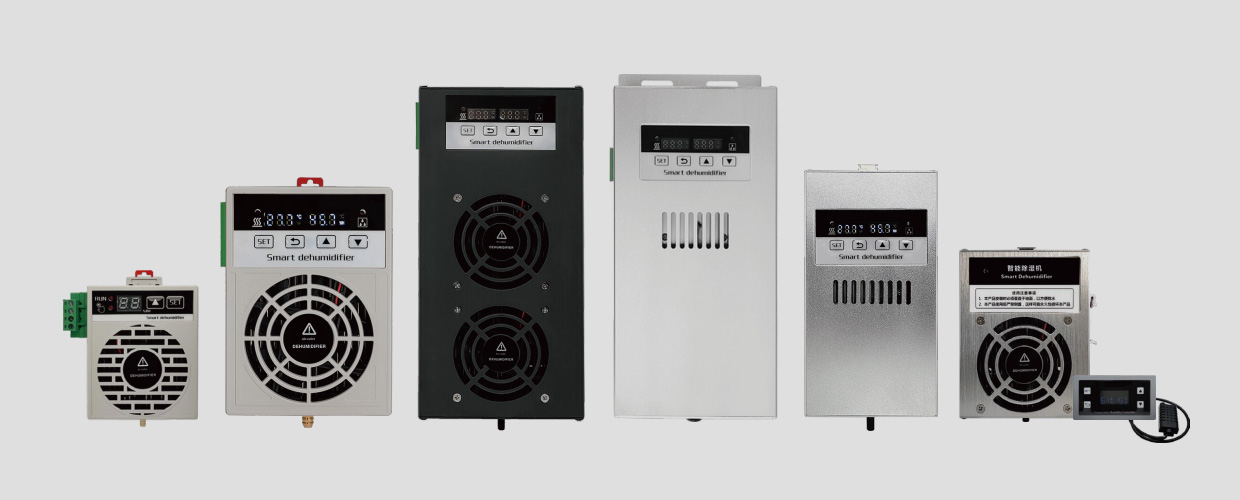
NOXT cabinet dehumidifiers stop condensation in electrical enclosures, storage cabinets and base stations. 40W to 120W, CE & RoHS, RS485 available.
Condensation inside an electrical cabinet is a quiet killer. It corrodes terminals, shorts control boards and causes failures that are expensive to trace. NOXT cabinet dehumidifiers solve this at the source with semiconductor condensation: no compressor, no refrigerant, no moving parts to wear out.
The range starts at a compact 40W model for small distribution boards and reaches a 120W stainless steel version for industrial cabinets and offshore towers. RS485 Modbus RTU is available on selected models, so a BMS or SCADA system reads cabinet humidity without anyone opening the door. Power options cover DC12V, DC24V and AC220V. Every unit ships with a datasheet, test report and a three-year warranty, and OEM branding starts at 100 pieces.
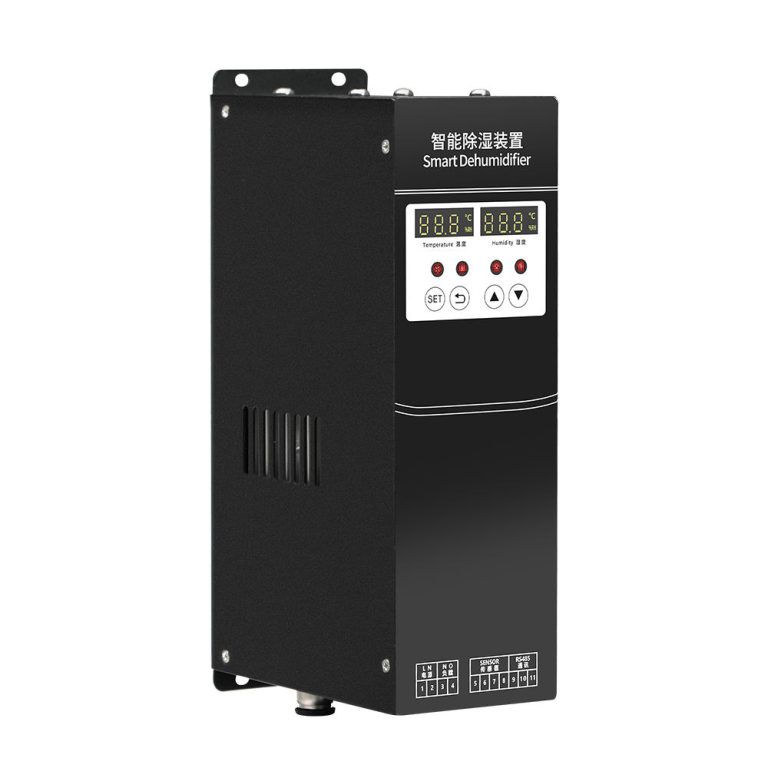
CSSU060 is a high‑performance industrial control module designed for cabinet temperature and humidity management. It delivers stable and reliable automatic monitoring and control, widely adopted in electrical cabinets, switchgear, automation enclosures and telecom equipment shelters. Built with robust hardware and intelligent logic, the CSSU060 accurately detects ambient temperature and humidity, and automatically activates heating or […]
CZCS1000 Intelligent Cabinet Dehumidifier is specially designed for industrial electrical enclosures, switch cabinets and control cabinets. It eliminates condensation, damp and corrosion inside cabinets, preventing short‑circuit and equipment aging caused by high humidity. Built on reliable semiconductor condensation technology, this compact dryer delivers stable dehumidifying performance without refrigerant.
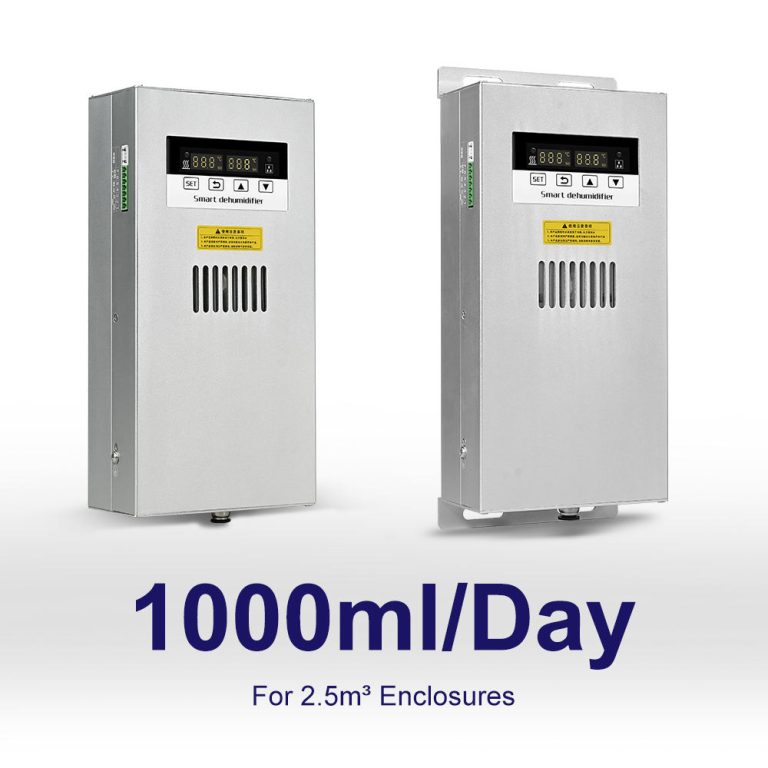
The CZ‑CS1000A smart dehumidifier adopts advanced semiconductor condensation technology, specially designed for electrical cabinets, control enclosures and other confined spaces. Built with an anodized aluminum housing, it delivers outstanding heat dissipation and long‑term durability. With a daily moisture removal capacity over 1000ml, it efficiently eliminates condensation, damp and water vapor, preventing circuit corrosion, short‑circuits and […]
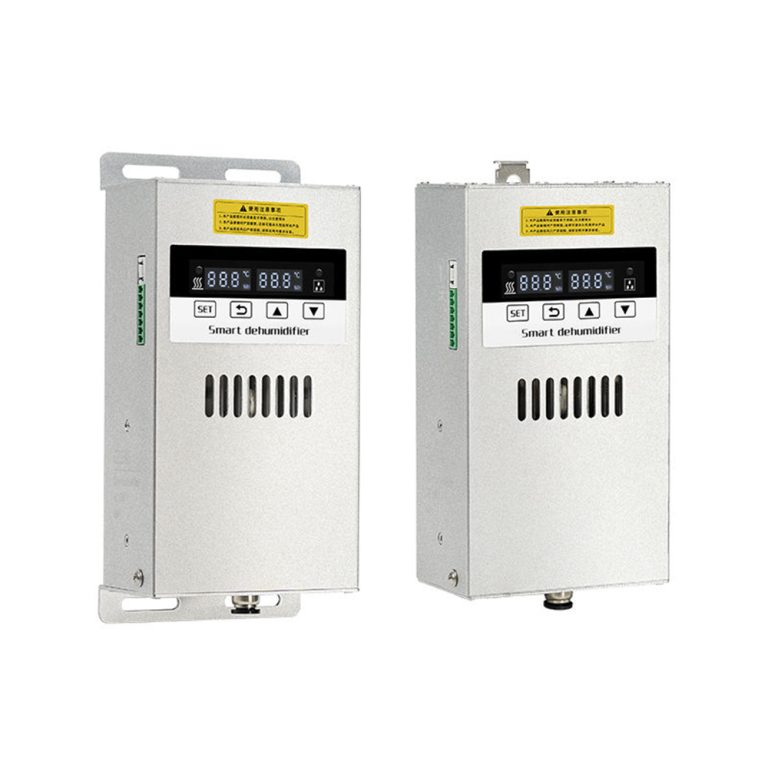
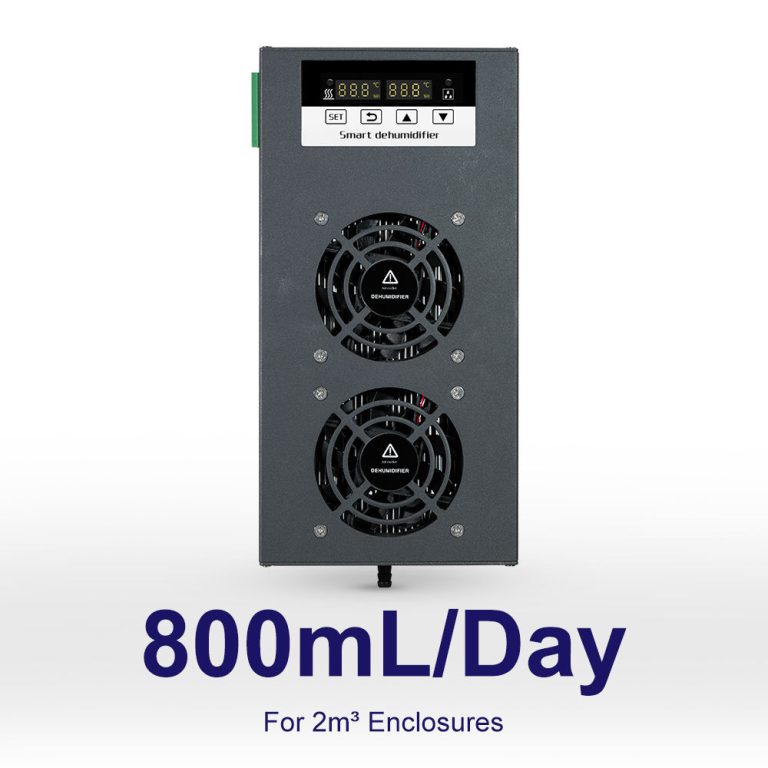
CZCS345 is an intelligent semiconductor cabinet dehumidifier specially developed for industrial enclosures. Adopting advanced semiconductor condensation technology, it effectively eliminates moisture and prevents internal condensation, rust and short‑circuit failures of electrical components. The unit features an anodized aluminum housing with excellent heat dissipation and long‑term durability. Equipped with a dual‑fan cooling system, LED digital display […]
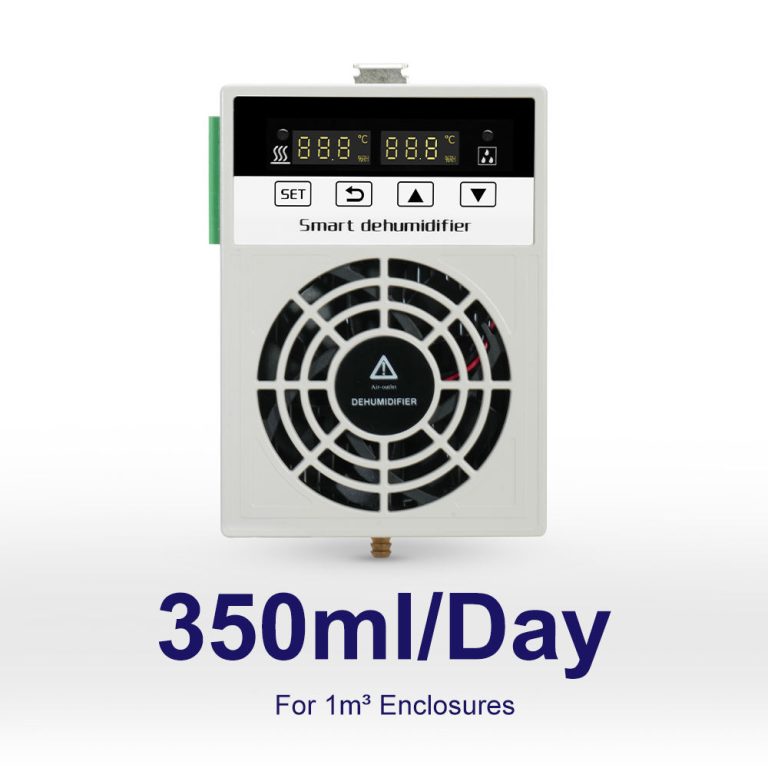
CZCS860 smart cabinet dehumidifier is specially designed for industrial enclosures. It adopts semiconductor condensation technology to reliably eliminate moisture inside electrical cabinets, prevent condensation, corrosion and short‑circuit faults, and protect valuable electrical components from damp damage.
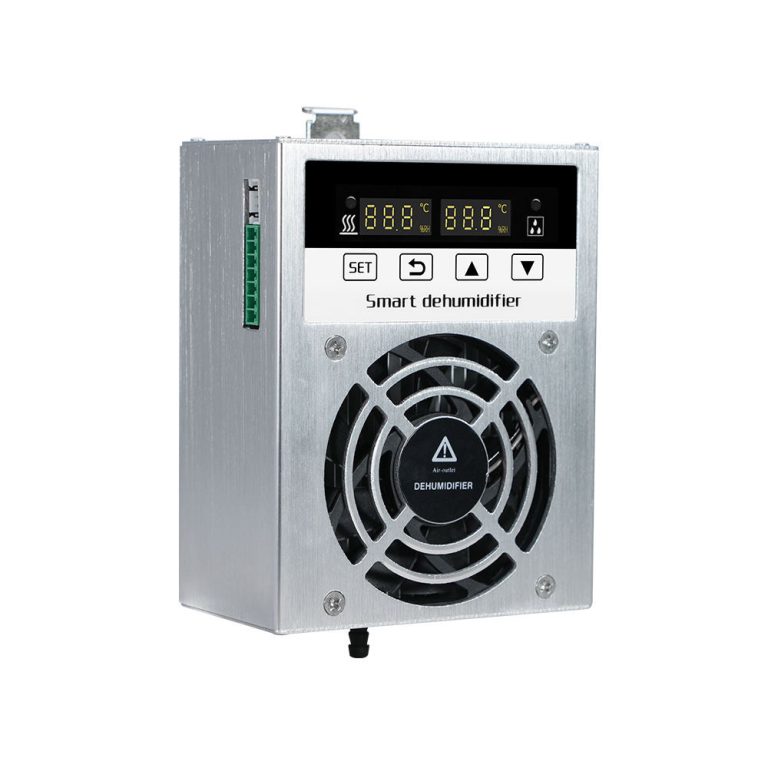
CZCS860A intelligent cabinet dehumidifier is designed for industrial electrical enclosures. It adopts semiconductor condensation technology to eliminate internal moisture, prevent condensation, corrosion and short‑circuit faults, and protect circuit breakers, controllers and precision electrical components. The brushed aluminum housing provides excellent heat dissipation and durability. With DIN‑rail mounting, RS‑485 remote communication and passive contact output, it […]
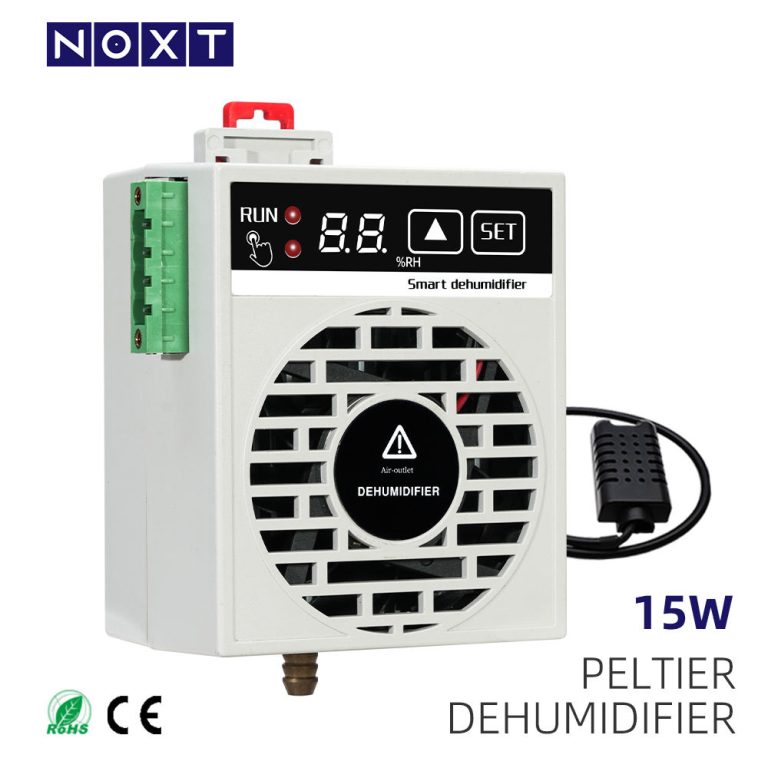
The CZCS880 intelligent cabinet dehumidifier is specially designed for industrial enclosures. It adopts advanced semiconductor condensation technology to effectively reduce internal humidity, prevent condensation, mold and corrosion, and protect electrical components from moisture damage. Equipped with an LED digital display and simple button operation, it supports real‑time humidity monitoring and precise humidity setting. The 35mm […]
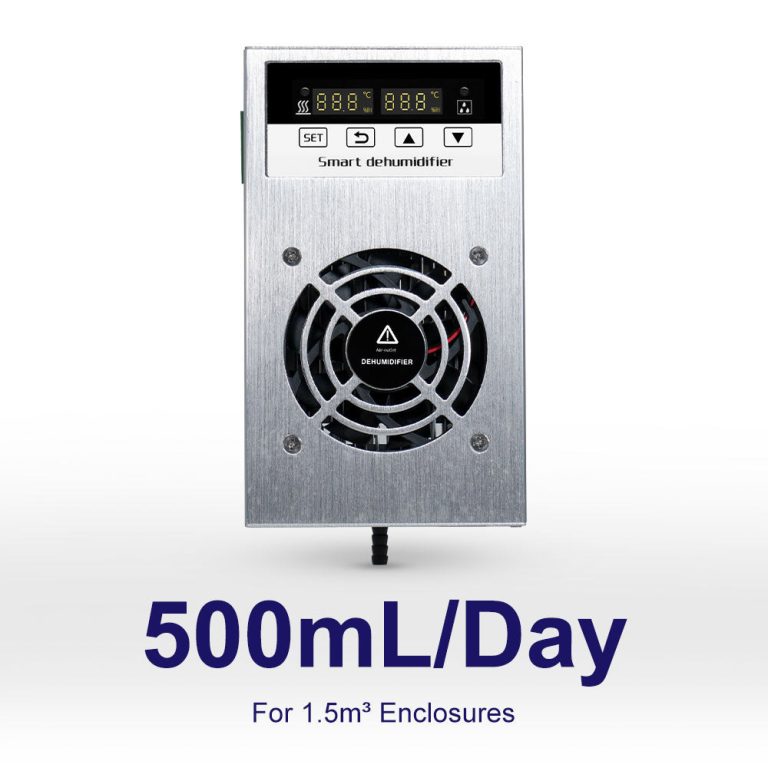
CZCS960A is an intelligent cabinet semiconductor dehumidifier specially designed for industrial enclosures. Adopting Peltier condensation cooling technology, it efficiently eliminates moisture inside electrical cabinets to prevent circuit corrosion, short circuits and condensation damage. The brushed aluminum housing delivers excellent heat dissipation and long‑term durability. Equipped with LED digital dual display and intelligent humidity & temperature […]
The single most important number is the internal volume of the cabinet, measured in liters. A distribution board of 200L needs far less moisture removal than a 600L storage cabinet. As a rule of thumb: cabinets up to 300L need a 60-80W unit (CZCS860, CZCS860A or CZCS345), while 300-800L enclosures need 120W (CZCS-120W or DSU021). For very large cabins measured in cubic meters, multiple units are recommended rather than a single oversized one, because air must circulate across the whole interior.
Indoor switchgear rooms and outdoor cabinets face very different conditions. For standard indoor electrical cabinets, a compact semiconductor unit is usually sufficient. For coastal, offshore, substation or high-humidity sites, choose a model with higher extraction capacity, corrosion-resistant housing and a wider operating temperature range. Stainless steel construction is recommended where salt spray, chemical vapors or wash-down maintenance are expected. Always match IP rating, power input (DC12V, DC24V or AC220V) and mounting space to the actual installation environment.
If the cabinet is inspected manually on a regular schedule, a standalone dehumidifier without communication may be enough. For substations, RMUs, smart grid cabinets, offshore towers and unmanned sites, remote monitoring saves cost and reduces the risk of undetected moisture damage. Selected NOXT models offer RS485 Modbus RTU, allowing humidity and operating status to be read by a BMS or SCADA system without opening the cabinet door. Remote monitoring is especially valuable when many cabinets are spread across a site and early warning is needed before condensation affects terminals or control boards.
Before selecting a model, confirm the available mounting area, door clearance and airflow path inside the cabinet. Semiconductor dehumidifiers have no compressor, refrigerant or wearing mechanical parts, so maintenance is typically limited to periodic cleaning of the condensing surface and checking the drain path. Narrow cabinets may need a split-type or front-mount design, while larger enclosures can accept a higher-capacity unit with greater daily extraction. Planning maintenance access at the specification stage avoids costly rework after installation.
If cabinet volume, environment, power supply and monitoring requirements are known, NOXT engineering can confirm the most suitable model, datasheet and lead time. Provide the enclosure volume in liters, installation location, desired communication option and available power source. For OEM projects, branding and batch quantities can also be discussed from 100 pieces upward. A confirmed specification ensures the correct dehumidifier is selected before purchase, with datasheet, test report and warranty details included.
Test report per batch
Datasheet + test report
CADs, logos, test reporting
1-5 pcs for qualified buyers
Between 350ml and 600ml per day depending on the model, measured at 30C/80%RH. CZCS345 removes 500ml/day, CZCS-120W removes 600ml or more.
Yes. Operating range is -20C to +60C. With no compressor, cold-climate performance stays stable.
Yes on CZCS860A, CZCS345 and CZCS1000A (Modbus RTU). Humidity can be read remotely and alerts triggered without opening the cabinet.
DC12V, DC24V and AC220V. DC versions fit solar storage cabinets and telecom sites with DC buses.
Yes. Custom colors, logos and packaging, MOQ 100 pcs. Every order ships with datasheet and CE/RoHS certificates.